

MOTEK Screening and Crushing Bucket Redefines the Paradigm for Efficient Calcite Processing
Release time: 2026-09-22
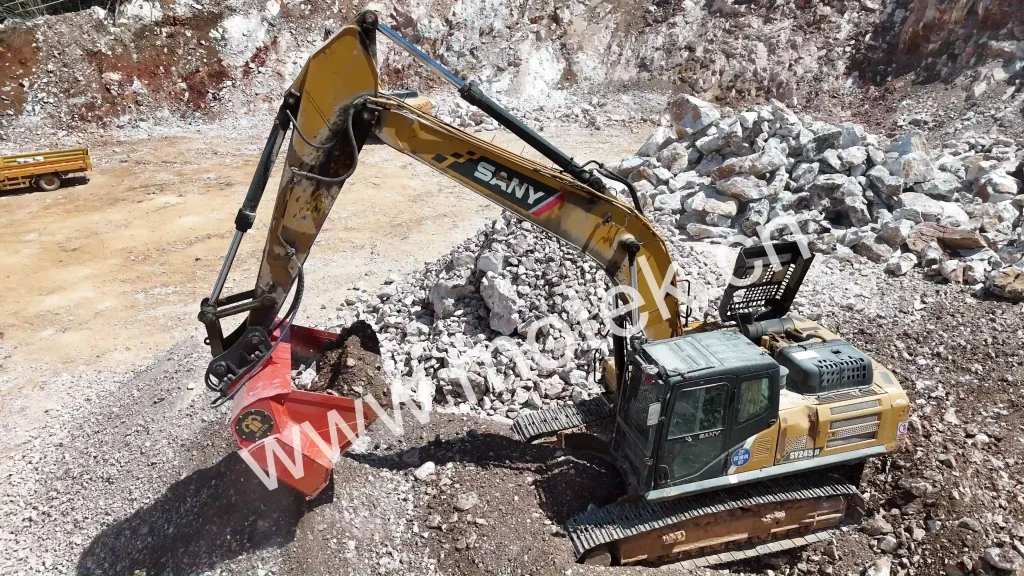
As a widely distributed calcium carbonate mineral, calcite has become an indispensable core raw material in the industrial sector, thanks to its high whiteness, fine texture, moderate hardness, and chemical stability. From high-end coatings, plastic fillers, papermaking powders, and pharmaceutical excipients to construction stone, cement raw materials, and metallurgical additives, the quality of calcite processing directly determines the grade and market value of the final products. In the aggregate and mineral processing industry, the core objectives of calcite processing consistently focus on three aspects: uniform particle size without oversized particles, high powder purity free from impurities, and low processing costs combined with high product utilization rates.
However, traditional calcite processing methods have long been plagued by industry pain points that severely constrain the production capacity and profitability of mines and stone processing plants. Conventional fixed crushing and screening lines rely on bulky equipment that requires a large footprint and incurs high relocation costs, making them ill-suited for scenarios involving scattered mining sites, open-pit operations, or space-constrained environments. These systems utilize multi-stage, sequential operations—involving jaw crushers, screens, and conveyors—that are cumbersome and highly energy-intensive. Furthermore, because calcite is relatively brittle, traditional high-force crushing equipment often causes over-crushing and produces an excess of needle-like or flaky particles; this results in substandard finished products and significant waste of high-quality ore. Additionally, moist raw material tends to clog traditional screens, causing screening efficiency to plummet and necessitating frequent equipment downtime for maintenance, which drives up labor costs and severely disrupts operational schedules.
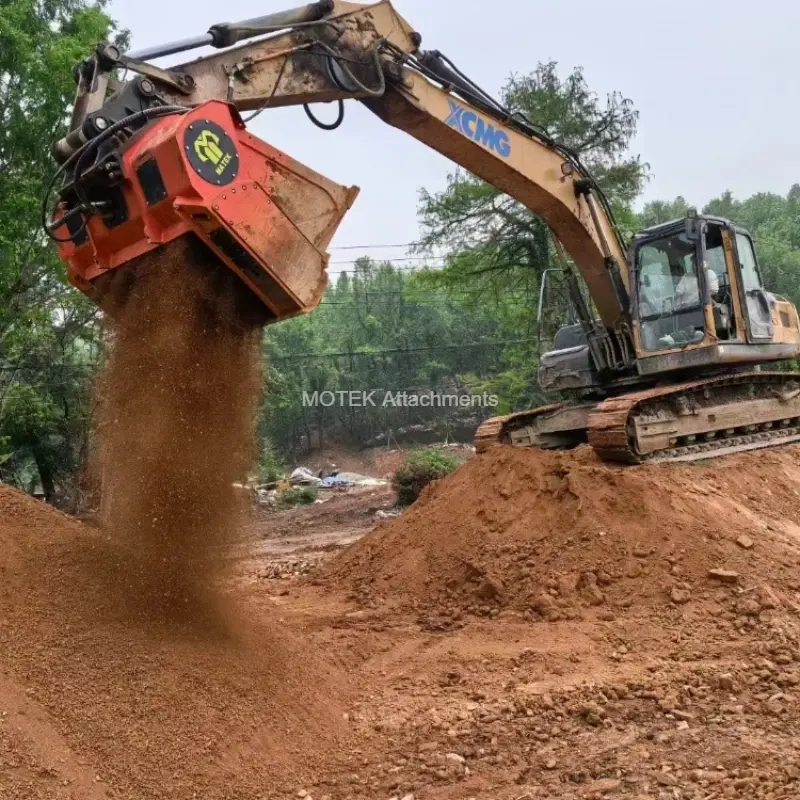
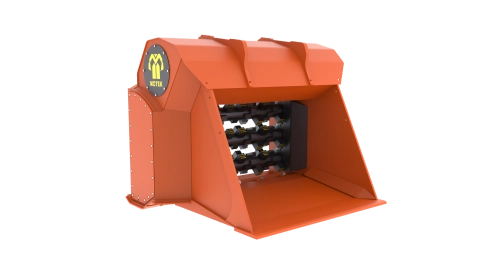
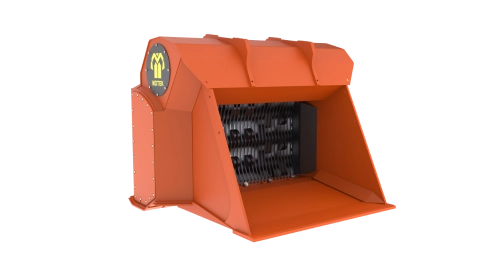
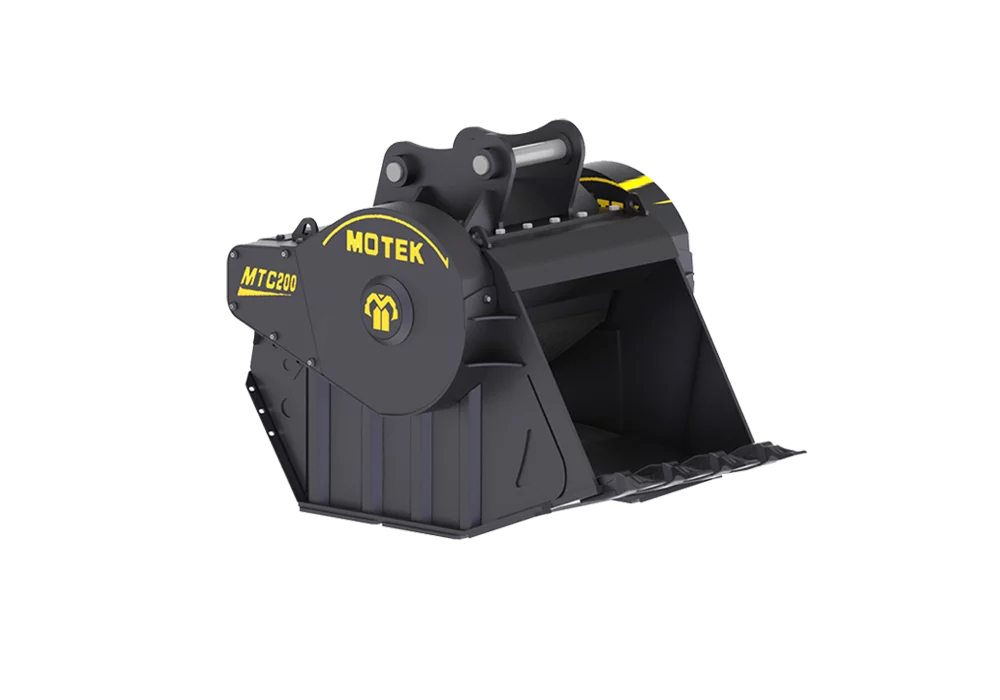
To address these industry challenges and the demand for precision processing, MOTEK’s screening and crushing bucket breaks the limitations of traditional equipment through its innovative integrated design, specialized mineral-adaptation technology, and robust industrial-grade durability. Combining crushing, screening, grading, and mixing capabilities into a single unit, it serves as a core solution for open-pit calcite mining, on-site processing, and precision material production. It empowers mining enterprises, stone processors, and construction teams with a low-cost, high-capacity, and high-quality processing solution, fundamentally revolutionizing the operational model for calcite crushing and screening.
Traditional calcite processing relies on fixed production lines characterized by high equipment procurement costs, lengthy installation times, and extremely poor mobility; such systems lack the flexibility needed for scenarios involving scattered mountain deposits, on-site construction waste, or the reprocessing of existing stockpiles. Multi-stage processing operations not only require extensive manual coordination and material transfer but also lead to issues such as material loss, dust pollution, and project delays. In contrast, MOTEK screening and crushing bucket—leveraging the core advantage of replacing an entire production line with a single unit—perfectly meets the processing needs of all calcite application scenarios, fundamentally resolving these persistent industry challenges.
Featuring a modular, integrated design, MOTEK rock screening bucket attaches directly to mainstream construction machinery—such as excavators and loaders—without complex modifications. It offers rapid installation and immediate operational readiness, allowing for on-the-go use and relocation, thereby completely eliminating constraints related to site, environment, or mine location. Whether for the primary processing of raw stone at open-pit mines, the recycling of calcite waste at processing plants, the pre-treatment of powdered raw materials at construction sites, or the precision processing of scattered ore, the bucket enables on-site crushing, screening, and shaping. This eliminates the cumbersome processes of material transport, stockpiling, and repeated loading and unloading, significantly reducing material loss and transportation costs.
In the mineral processing industry, cost control is the key to profitability. Traditional fixed production lines for calcite processing entail high costs for equipment procurement, installation, and maintenance, alongside high energy consumption and significant labor requirements—burdens that are often difficult for small and medium-sized mining enterprises to bear. Furthermore, such large-scale equipment often suffers from high idle rates, leading to substantial resource waste. MOTEK screening and crushing buckets—featuring a lightweight, integrated design, low energy consumption, and maintenance-free operation—significantly reduce the overall production costs of calcite processing, enabling enterprises to maximize their profits.
Compared to traditional multi-stage production lines, a single MOTEK screening and crushing bucket replaces multiple pieces of equipment—such as crushers, screeners, conveyors, and mixers—thereby directly reducing procurement costs. It eliminates the need for permanent factory buildings or structural steel frameworks and incurs no site modification expenses; installation and commissioning are quick, enabling rapid startup and revenue generation. Powered by the host machinery’s hydraulics, the unit requires no independent power supply and consumes far less energy than traditional stationary equipment, offering significant energy savings and reduced long-term electricity and fuel costs. Furthermore, its integrated operational design allows a single operator to control the entire unit, drastically cutting labor costs and streamlining the production process.
In terms of production capacity, MOTEK’s equipment features a large-volume hopper design paired with a high-efficiency crushing and screening structure; this enables high-volume batch processing and stable continuous operation, resulting in a capacity increase of over 30% compared to traditional processing methods. It achieves 100% recovery and reprocessing of materials such as calcite offcuts, tailings, and waste stone, transforming previously discarded, low-value materials into qualified raw materials; this significantly boosts ore utilization, minimizes resource waste, and turns waste into a valuable asset. Furthermore, the equipment drastically reduces the frequency of material transfer and lowers pollution from dust and spillage, meeting “green mine” environmental construction standards without the need for additional environmental protection equipment, thereby avoiding the risks associated with environmental compliance rectifications.
Mining operations take place in complex, harsh environments characterized by heavy dust, intense vibration, and demanding working conditions, placing extreme demands on equipment durability, stability, and adaptability. Leveraging advanced industrial manufacturing processes, MOTEK screening and crushing buckets hold numerous invention and utility model patents and have secured multiple authoritative certifications, including CE, workplace safety, and quality management system standards. The unit is forged from thickened, high-strength steel, while critical drive, crushing, and screening components utilize wear-resistant, anti-corrosive alloys. Engineered for impact, wear, and corrosion resistance, the equipment reliably withstands the rigors of open-pit mines, muddy terrain, and dust-laden areas, easily handling high-intensity, continuous operation.
The equipment features a unique belt-drive structure that effectively buffers the hydraulic system against crushing vibrations, thereby protecting the main unit and auxiliary machinery while extending the machine’s overall service life. It boasts an exceptionally low failure rate, requiring only routine cleaning and maintenance—eliminating the need for frequent overhauls or part replacements—and resulting in minimal operating and maintenance costs. Additionally, the equipment utilizes a universal connection interface compatible with the vast majority of excavators and loaders on the market; it requires no specialized modifications, allows for easy installation and flexible transport, and enables rapid relocation between job sites. It is perfectly suited for a wide range of applications, including calcite mining, deep processing at plant sites, on-site material blending, and the resource recovery of tailings.
Whether for large-scale, standardized batch processing at mines, small-scale, precision production at scattered sites, calcite waste recycling, or on-site material processing at construction projects, MOTEK screening and crushing buckets consistently deliver high-quality finished products. Balancing productivity, quality, cost-efficiency, and flexibility, they serve as a key tool for reducing costs, increasing efficiency, and driving industrial transformation and upgrading within the calcite processing sector.
As the mineral industry evolves toward greater precision, sustainability, and efficiency, the extensive processing model is gradually being phased out in favor of high-quality, cost-effective, and eco-friendly methods. For calcite—a high-value-added industrial raw material—market competitiveness is directly determined by the quality, particle size precision, and purity of the finished product. Addressing key pain points in the mineral processing sector, MOTEK’s screening and crushing bucket optimizes the calcite processing workflow. By leveraging core advantages such as integrated functionality, precise control, high operational efficiency, and low maintenance costs, it resolves the issues of low output, poor quality, high costs, and limited flexibility often associated with traditional equipment.
For years, MOTEK has been deeply committed to the fields of engineering equipment and mineral processing. Backed by mature technical expertise, rigorous quality control, and comprehensive after-sales support, our products are exported worldwide and have earned high acclaim from countless mining enterprises and construction teams. We provide dedicated, one-stop service—covering everything from equipment customization, installation, and commissioning to technical guidance, repairs, maintenance, and upgrades—ensuring a worry-free experience for our customers from purchase through operation.
Leave behind the cumbersome and inefficient traditional processing methods and embrace a new era of intelligent, high-efficiency, precision production! Choose the MOTEK screening and crushing bucket to replace an entire production line with a single unit. Unlock a new, profitable model for calcite processing—featuring lower investment, reduced energy consumption, higher output, and superior quality—that empowers enterprises to gain a competitive edge, achieve efficient production, boost green revenue, and ensure long-term growth.
Author
Lilly Liu
MOTEK Director of International Sales Equipped with 15 years of dedicated experience in the construction machinery industry, she has a deep understanding of global market dynamics and regional customer needs. She has successfully led teams to penetrate key international markets, particularly in promoting construction machinery attachments and securing high-value overseas orders.